
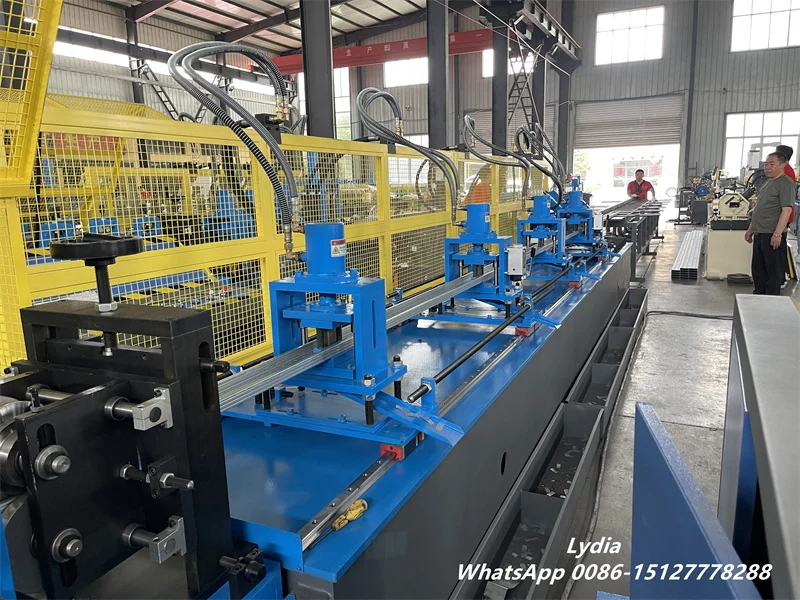
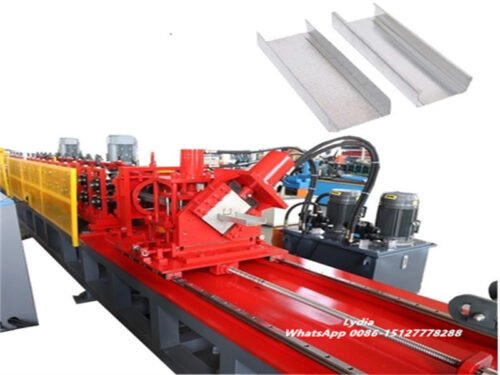
As the demand for lightweight steel construction continues to grow in the United States, manufacturers need reliable equipment to produce accurate metal studs and tracks for drywall framing systems. The C Stud and U Track Roll Forming Line is specially designed to manufacture galvanized steel framing profiles used in interior partition walls, commercial buildings, residential construction, and ceiling systems.
This automatic Drywall Framing Roll Forming Line processes G60 and G90 galvanized steel coils with thicknesses ranging from 0.4 to 1.0 mm. It supports different profile dimensions, including web widths from 41 to 152 mm, 32 mm flanges, and adjustable lips from 6 to 10 mm. With automatic size adjustment, hydraulic punching, and servo tracking cutting, the production line helps manufacturers improve productivity while maintaining consistent profile accuracy.
1. What Is a C Stud and U Track Roll Forming Machine?
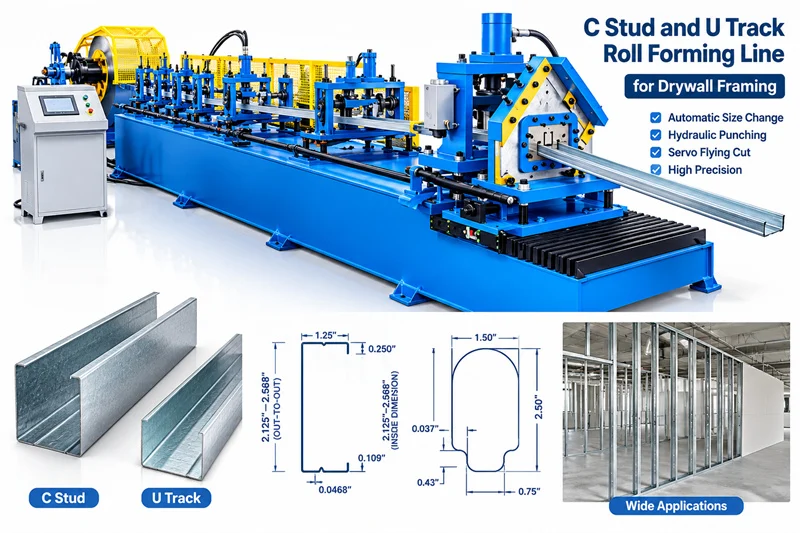
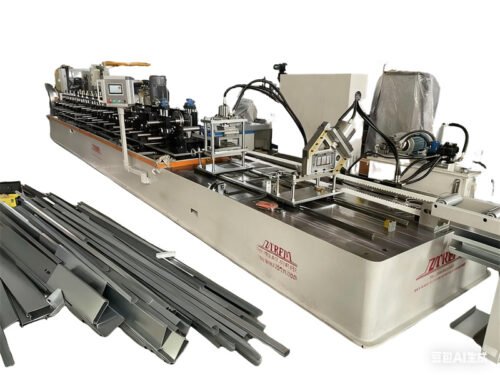
A C Stud and U Track Roll Forming Machine is an automated metal forming system that produces C-shaped steel studs and U-shaped steel tracks from galvanized steel coils. These profiles are essential components of modern drywall framing systems.
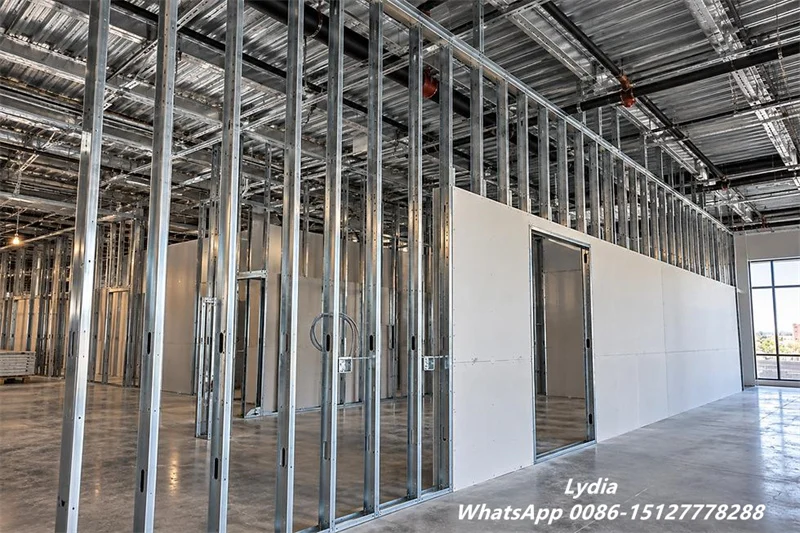
C studs are commonly installed vertically as structural members inside partition walls, while U tracks serve as horizontal channels at the top and bottom of the framing structure. Together, they create a stable framework for installing gypsum boards, insulation materials, and interior wall panels.
Unlike conventional manufacturing equipment that requires extensive manual adjustments, this automatic metal stud and track machine can change profile dimensions through a motorized or servo-driven adjustment system. Operators can select the required specifications through the control panel, reducing setup time and improving production flexibility.
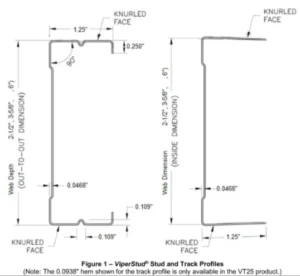
2. Profile Specifications for the US Drywall Framing Market
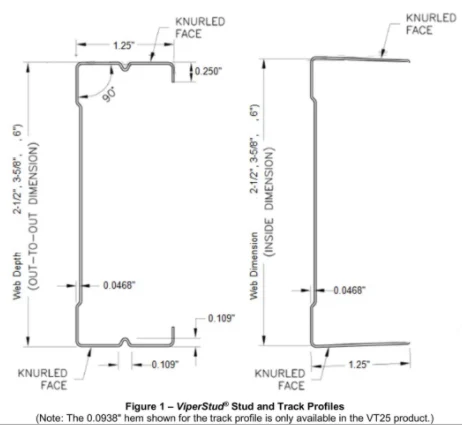
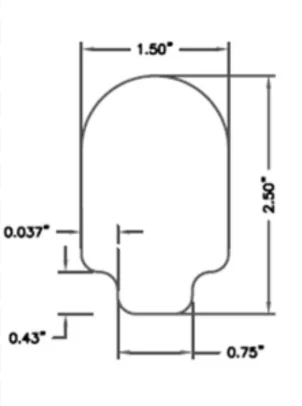
The production line is designed around common North American drywall framing requirements. It can manufacture different C stud and U track profiles by adjusting the web width, flange dimensions, and lip configuration.
| Profile Parameter | Specification |
|---|---|
| Profile Types | C Stud and U Track |
| Web Width | 41–152 mm (1-5/8 to 6 inches) |
| Flange Width | 32 mm |
| Adjustable Lip | 6–10 mm |
| Material | Galvanized Steel G60 / G90 |
| Material Thickness | 0.4–1.0 mm |
| Yield Strength | Up to 485 MPa (70 ksi) |
| Size Adjustment | Automatic Motorized or Servo Adjustment |
| Optional Function | Flange Knurling (Embossing) |
The machine can be configured for different framing dimensions according to the customer’s profile drawings. Its automatic width adjustment system eliminates the need for manual spacer replacement during routine size changes. This design is particularly useful for manufacturers supplying multiple stud and track sizes to the US construction market.
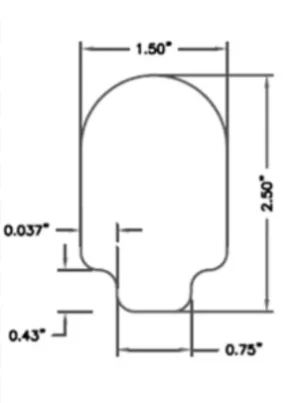
3. Automatic Size Change System for Multiple Profiles
Production flexibility is an important consideration for drywall framing manufacturers. Different construction projects require different stud widths and track dimensions, so frequent manual machine adjustments can reduce production efficiency.
Our automatic C stud and U track roll forming line can integrate a motorized or servo-driven size adjustment system. The operator selects the target profile dimensions through the PLC touchscreen, and the machine automatically adjusts the corresponding forming components.
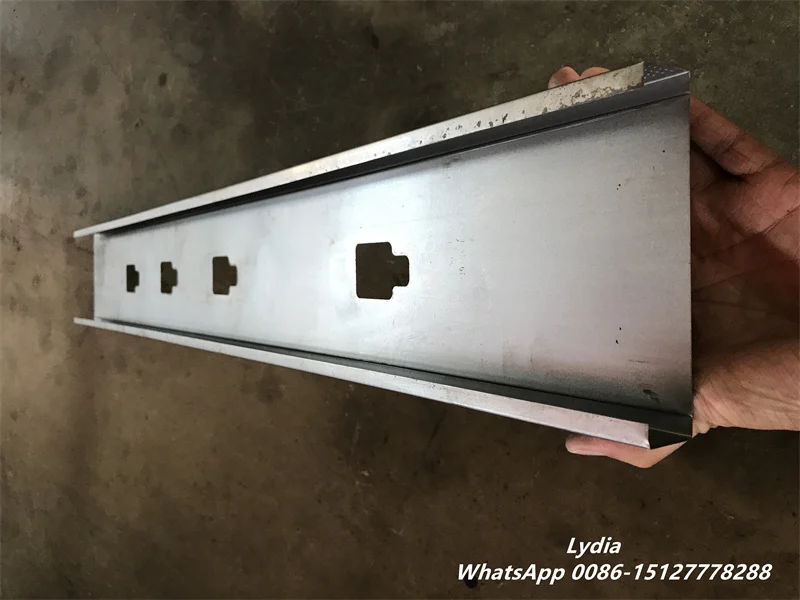
Depending on the final machine configuration, the adjustment system can support:
- Automatic adjustment of different web widths.
- Quick changeover between C stud and U track production.
- PLC-based parameter storage for repeat production orders.
- Reduced manual adjustment and setup time.
This system allows one production line to manufacture a wider range of drywall framing profiles. The final adjustment range and compatibility between C stud and U track configurations will be confirmed according to the customer’s drawings.
4. High-Precision Rollers and Gearbox Drive System
When processing galvanized steel with yield strength up to 485 MPa, the roll forming machine must provide sufficient rigidity and stable transmission. The mechanical design directly affects profile accuracy, forming consistency, and equipment service life.
For this metal stud and track roll forming machine, we recommend a gearbox-driven transmission system for customers who prioritize stable operation and reliable power transfer.
| Machine Component | Recommended Configuration |
|---|---|
| Drive System | Gearbox Drive (Preferred) |
| Alternative Drive | Chain Drive (Optional) |
| Roller Material | Cr12MoV |
| Roller Hardness | HRC 58–62 |
| Shaft Material | 45# Steel |
| Shaft Treatment | Quenching and Tempering |
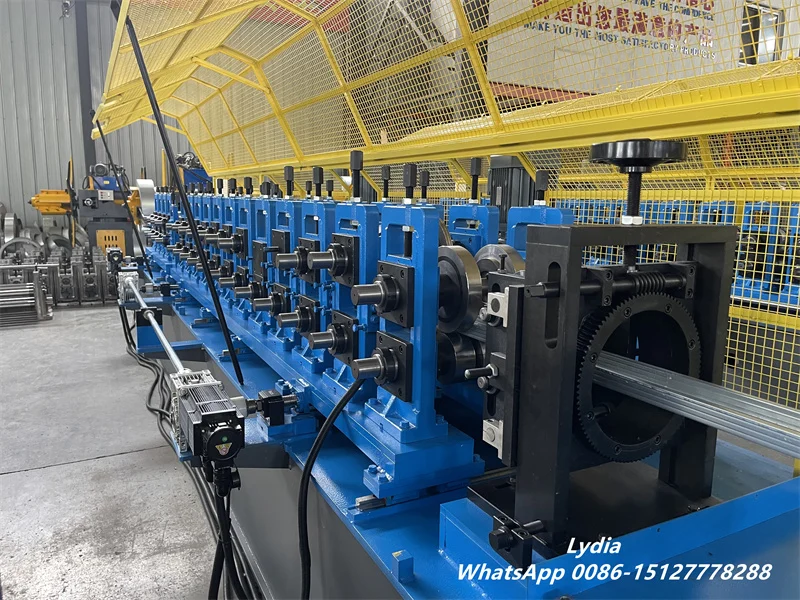
Cr12MoV hardened rollers provide excellent wear resistance and forming stability. The 45# steel shafts undergo quenching and tempering to improve mechanical strength and support continuous production. Compared with a chain-driven arrangement, the gearbox option offers a more integrated transmission structure and is worth considering for demanding production schedules.
5. Hydraulic Punching and Non-Stop Servo Flying Cutting
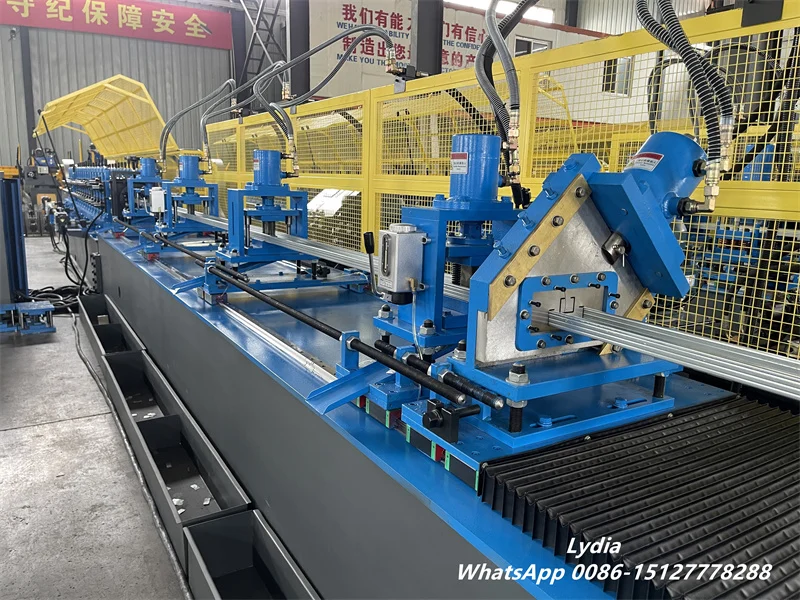
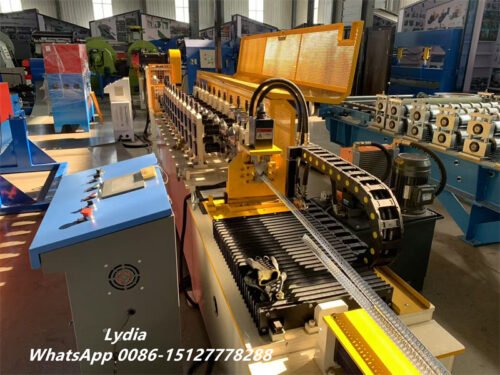
Drywall framing profiles often require service holes for electrical wiring, plumbing, and other building installations. The C stud roll forming machine can integrate hydraulic punching stations to produce service holes at specified positions.
The punching layout, hole dimensions, and spacing can be customized according to the customer’s profile drawings and application requirements. Hydraulic punching provides a practical solution for processing different hole patterns during continuous production.
For finished profile cutting, the production line uses a servo tracking flying cut system. Instead of stopping the entire forming line before every cut, the cutting carriage synchronizes with the moving profile and completes the cutting operation while the material continues to advance.
- Cutting Method: Servo tracking flying cut.
- Production Mode: Non-stop continuous forming and cutting.
- Length Tolerance: ±1 mm under agreed operating conditions.
- Cutting Control: PLC and servo synchronization.
- Cutting Length: Programmable according to production requirements.
This configuration reduces unnecessary production interruptions and helps maintain consistent cutting lengths. The actual cutting accuracy depends on material properties, profile dimensions, machine calibration, and operating conditions.
6. Main Machine Configuration and Technical Specifications
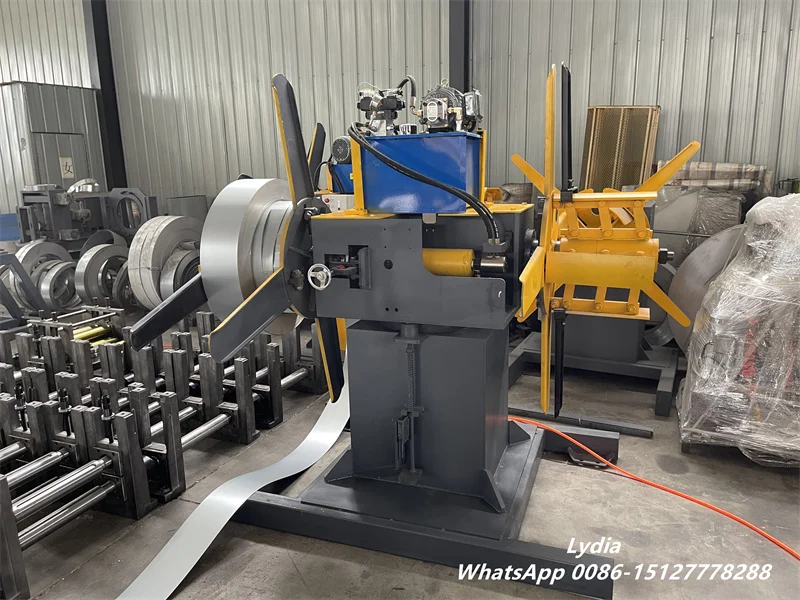
The complete Drywall Framing Roll Forming Production Line can include a decoiler, feeding and leveling section, hydraulic punching unit, roll forming system, servo tracking cutting unit, and PLC control system.
| Item | Technical Specification |
|---|---|
| Applicable Material | G60 / G90 Galvanized Steel |
| Material Thickness | 0.4–1.0 mm |
| Maximum Yield Strength | 485 MPa (70 ksi) |
| Profile Type | C Stud / U Track |
| Web Width | 41–152 mm |
| Flange Width | 32 mm |
| Lip Width | 6–10 mm, Adjustable |
| Forming Stations | To Be Confirmed According to Profile Design |
| Forming Speed | To Be Confirmed According to Punching and Profile Requirements |
| Drive System | Gearbox / Chain Drive |
| Roller Material | Cr12MoV, HRC 58–62 |
| Shaft Material | 45# Steel, Quenched and Tempered |
| Punching System | Hydraulic Punching |
| Cutting System | Servo Tracking Flying Cut |
| Cutting Tolerance | ±1 mm |
| Decoiler Capacity | 3 Tons |
| Decoiler Type | Manual or Hydraulic |
| Control System | PLC with Touchscreen |
The final number of forming stations and production speed will be determined after reviewing the complete C stud and U track profile drawings. This ensures that the machine configuration matches the actual material thickness, steel strength, profile geometry, and required punching operations.
7. Optional Flange Knurling and Customized Functions
For manufacturers who require additional profile features, the C stud and U track machine can be equipped with optional flange knurling, also known as embossing or ambushing in some industry specifications.
This process creates a textured pattern on the flange surface according to the required design. It can help provide additional surface characteristics for specific framing applications. The knurling pattern, position, and tooling arrangement should be confirmed using the customer’s sample or technical drawing.
We can provide a separate quotation for the flange knurling function, allowing customers to compare the standard machine configuration with the upgraded version.
Other optional configurations include:
- Hydraulic decoiler with automatic coil expansion.
- Gearbox-driven transmission system.
- Servo-driven automatic width adjustment.
- Customized hydraulic punching patterns.
- Additional profile-specific tooling and cutting arrangements.
8. Why Choose Our Drywall Framing Roll Forming Line?
For manufacturers serving the US metal framing industry, production flexibility and consistent profile quality are essential. Our Drywall Framing Roll Forming Line can be engineered around North American stud and track dimensions, galvanized steel grades, and customer-specific production requirements.
- US Market Compatibility: Designed for common North American C stud and U track profile dimensions.
- High-Strength Material Processing: Configurable for galvanized steel with yield strength up to 485 MPa.
- Automatic Size Change: Motorized or servo-driven adjustment without manual spacer replacement.
- Stable Transmission: Gearbox drive available for demanding industrial production.
- Precision Forming: Hardened Cr12MoV rollers and treated steel shafts.
- Continuous Production: Servo tracking flying cut minimizes production interruptions.
- Customized Punching: Hydraulic punching layouts designed around service hole requirements.
- Flexible Configuration: Optional flange knurling and manual or hydraulic decoiler.
9. Frequently Asked Questions About C Stud and U Track Roll Forming Machines
Q1: Can one machine produce both C studs and U tracks?
Yes. One production line can be configured to manufacture both C studs and U tracks. The machine uses an automatic size adjustment system and profile-specific forming arrangements. The exact changeover capability depends on the approved profile drawings and machine design.
Q2: Can the machine process G60 and G90 galvanized steel?
Yes. The production line can be designed for G60 and G90 galvanized steel with thicknesses from 0.4 to 1.0 mm. It can also be engineered for yield strength up to 485 MPa (70 ksi), subject to final material specifications and forming calculations.
Q3: Does the machine support automatic size adjustment?
Yes. A motorized or servo-driven adjustment system can automatically change the required profile dimensions. It avoids manual spacer replacement and helps reduce setup time when switching between different stud and track sizes.
Q4: What is the difference between gearbox drive and chain drive?
Gearbox drive provides an integrated transmission structure and is recommended for customers who prioritize stable operation and robust mechanical performance. Chain drive is an alternative configuration with a different transmission and maintenance arrangement. Both options can be evaluated according to the production requirements and budget.
Q5: Can the machine cut profiles without stopping production?
Yes. The servo tracking flying cut system synchronizes the cutting carriage with the moving steel profile. This allows the machine to perform cutting during continuous production, with a target length tolerance of ±1 mm under agreed operating conditions.
Get a Customized C Stud and U Track Roll Forming Machine Quotation

Reviews
There are no reviews yet.